2026 Top Pneumatic Punching Machine Buying Guide
The 2026 Top Pneumatic Punching Machine Buying Guide is designed for manufacturers comparing speed, accuracy, safety, and operating cost. A pneumatic punching machine converts compressed air into controlled punching force, making it useful for sheet metal, electrical cabinets, hardware parts, and light fabrication. The right model should feel predictable at the workbench, not merely impressive in a brochure.
Industry evidence supports a careful evaluation. The U.S. Department of Energy reports that compressed air can represent a significant share of industrial electricity use, while leaks and poor maintenance can waste substantial energy. Small leaks matter. Grand View Research’s metal stamping market analysis also identifies automation, higher production efficiency, and consistent forming quality as important market drivers. These trends explain why buyers increasingly examine cycle time, air consumption, die compatibility, and control systems together.
This guide combines practical workshop experience with manufacturer specifications and recognized industry research. It explains how to compare throat depth, punching capacity, stroke length, repeatability, noise, guarding, and maintenance access. OSHA machine-guarding principles should remain part of the purchasing decision, especially where operators load flat stock by hand. A lower purchase price may hide costly compressor demand, frequent seal replacement, or difficult tooling changes. Reality is messier. Some published performance figures depend on material grade, sheet thickness, air pressure, and testing conditions. Buyers should request sample trials, service records, warranty terms, and measured energy data before committing. A reliable machine is not simply fast; it produces clean holes repeatedly, protects operators, and remains serviceable after years of daily use.
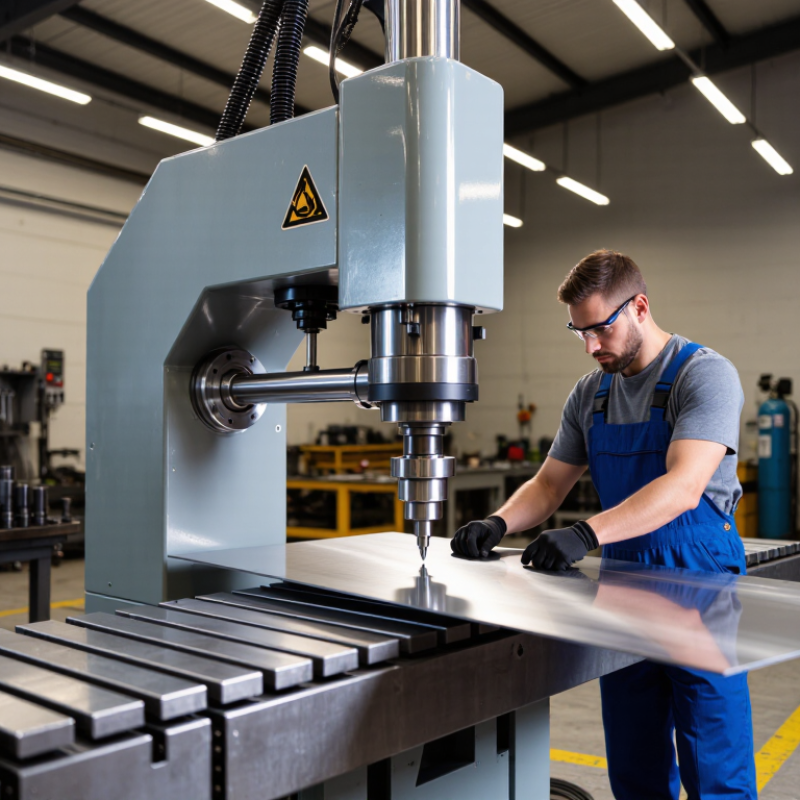
Pneumatic Punching Machines Explained: 0.4–0.8 MPa Air-Pressure Basics
2026 Top Pneumatic Punching Machine Buying Guide
Pneumatic Punching Machines Explained: 0.4–0.8 MPa Air-Pressure Basics
In 2026, pneumatic punching machine selection starts with air pressure, not advertising claims. Most workshop systems operate between 0.4 and 0.8 MPa. That range describes supply pressure at the inlet. It does not guarantee punching force. A regulator, hose, filter, and valve can reduce pressure before the cylinder works. Check the gauge during a real cycle. Static readings can mislead. I have seen a machine show 0.8 MPa, then weaken because the compressor could not maintain flow.
At 0.4 MPa, lighter sheet materials and smaller dies may punch consistently. Thicker stock usually needs more force, better die clearance, or slower cycling. Raising pressure blindly can damage seals, distort holes, and increase wear. The cylinder bore matters because force roughly equals pressure multiplied by piston area.
Air consumption matters too. A narrow hose may starve the actuator during repeated strokes. Keep the material, thickness, hole diameter, and cycle rate beside the machine specification.
Before buying, request test results using your own material. Measure hole quality, burrs, noise, and recovery time between strokes. Clean, dry air protects valves and supports stable operation. Follow the stated maximum pressure. Never exceed it to solve a sizing mistake. I would also inspect emergency controls and guarding. My earlier assumption was that higher pressure meant faster work. It did not. Consistent airflow and correct tooling often mattered more.
Calculate Required Punching Force: F ≈ L × t × Shear Strength
2026 Top Pneumatic Punching Machine Buying Guide
Calculate Required Punching Force: F ≈ L × t × Shear Strength
In 2026, pneumatic punch selection should begin with force, not advertised speed. The working estimate is F ≈ L × t × τ. Here, L is the total cutting perimeter, t is sheet thickness, and τ is material shear strength. Use consistent units. Millimetres and newtons per square millimetre produce newtons. This prevents costly undersizing.
Consider a 120 mm cutting perimeter in 2 mm low-carbon steel. Using τ = 300 N/mm², F ≈ 120 × 2 × 300 = 72,000 N, or 72 kN. Engineering tables in ASM Handbook, Volume 14B, commonly place low-carbon steel shear strength near 250–400 MPa, depending on grade and condition. Published ranges vary. Material certificates are better than guesses. Machinery’s Handbook also supports using material-specific shear values instead of tensile strength.
Add allowance for friction, stripping, misalignment, and tool wear. A practical starting factor is 1.2 to 1.5, although complex tooling may demand more. For this example, 72 kN × 1.3 equals 93.6 kN required capacity. Do not confuse cylinder force with usable punch force. Air pressure, piston area, stroke position, and regulator losses matter. Verify test results against ISO 6892-1 material data where possible. I would recalculate after production trials. Real sheets are less obedient than spreadsheets.
2026 Top Pneumatic Punching Machine Buying Guide - Calculate Required Punching Force: F ≈ L × t × Shear Strength
Basic calculation: F ≈ L × t × τ | F = theoretical punching force (N), L = total cutting or punching perimeter (mm), t = material thickness (mm), τ = material shear strength (N/mm² or MPa). The recommended machine force includes a 25% allowance for variation, friction, and tool wear.
Representative Pneumatic Punching Force Selection Data | Material | Typical Shear Strength
(MPa) | Punching Perimeter, L
(mm) | Material Thickness, t
(mm) | Theoretical Force
F = L × t × τ (kN) | Recommended Machine Force
Including 25% Allowance (kN) | Approx. Minimum Cylinder Bore at 0.6 MPa
and 85% Efficiency (mm) |
| Low-carbon steel | 300 | 80 | 2.0 | 48.0 | 60.0 | 122 |
| Stainless steel, austenitic grade | 500 | 50 | 1.5 | 37.5 | 46.9 | 108 |
| Aluminum alloy, heat-treated | 200 | 100 | 3.0 | 60.0 | 75.0 | 137 |
| Brass, cartridge-type alloy | 250 | 60 | 2.0 | 30.0 | 37.5 | 97 |
| Commercially pure copper | 210 | 75 | 1.5 | 23.6 | 29.5 | 86 |
| Galvanized low-carbon steel | 280 | 100 | 1.0 | 28.0 | 35.0 | 93 |
Engineering notes: Shear-strength figures are representative values for preliminary sizing; actual values vary with alloy, temper, hardness, rolling direction, and supplier specifications. The cylinder-bore estimate uses an effective pneumatic pressure of 0.6 MPa and 85% mechanical efficiency: D ≈ √[4F ÷ (π × p × η)]. Confirm the final selection using the actual material certificate, punch clearance, die geometry, operating pressure, and the machine manufacturer's safety requirements.
Compare Machine Capacity: 20–100 kN Force and 10–50 mm Stroke
For a 2026 pneumatic punching machine, capacity should match the material, hole size, and production rhythm. Force commonly ranges from 20 to 100 kN. A 20 kN model may suit thin aluminum, plastics, or light sheet work. Thicker steel usually requires higher force and stronger tooling. Do not select capacity by maximum force alone. Calculate the required load from material strength, thickness, and punch perimeter. Leave a practical margin for tool wear and inconsistent batches.
Stroke length typically ranges from 10 to 50 mm. A 10 mm stroke can deliver fast, controlled punching when the material sits close to the tool. A 50 mm stroke offers more clearance for stacked fixtures or deeper workpieces. It may also increase cycle time and air consumption. Longer is not automatically better. Check the die opening, tool entry, and return movement before deciding.
A useful shop-floor check is simple. Test several blanks from the actual material batch. Inspect hole edges, distortion, and slug removal. Listen for pressure drops during repeated cycles. One mistake is trusting a single successful sample. I have seen machines pass light trials, then struggle when production speed rises. A smaller machine with stable pressure may outperform a larger one operated near its limit. Record force, stroke, cycle rate, and air pressure during testing. Those details make later purchasing decisions more reliable.
Evaluate Buying Costs: Air Consumption, Cycle Speed, Tooling, and Maintenance
2026 Top Pneumatic Punching Machine Buying Guide
Buying cost extends far beyond the machine’s purchase price. Air consumption can quietly increase factory expenses. Check consumption at the working pressure, not only the advertised maximum. A machine using 0.4 cubic meters per minute may need a larger compressor during continuous production. Measure pressure at the machine inlet. Long hoses and small fittings can also reduce efficiency.
Cycle speed affects output, labor cost, and compressor demand. A rated 80 cycles per minute may fall to 55 with thicker sheet, longer strokes, or frequent positioning. Request a practical test using your material and actual tooling. Calculate output from usable cycles, not ideal cycles. Faster is not always cheaper. Sometimes it creates more rejects.
Tooling requires a realistic budget. Punches, dies, guides, and sharpening services should match your material thickness and hole size. Cheap tooling can wear quickly and damage finished parts. Maintenance usually includes filter inspection, seal checks, lubrication where specified, and alignment reviews. Keep replacement seals and critical springs nearby. A short service stop is cheaper than an unexpected production delay. My own buying mistake was trusting the catalog cycle rate too much. It looked precise, but the test conditions were missing. Ask for operating data, service intervals, noise readings, and spare-part availability in writing. The details matter.
