How to Get Better Welds with These Spot Welding Tips
A clean spot weld is small, but its quality depends on several tightly linked variables. Electrode force, welding current, weld time, surface condition, and part fit-up all shape the result. When one drifts, the joint may look sound while its strength changes. That is easy to overlook.
Automation makes consistency more important, not automatic. The International Federation of Robotics’ World Robotics 2024 report counted 4.28 million industrial robots operating worldwide in 2023, up 10 percent from the previous year. The figure describes factory automation broadly; it is not a spot-welding quality measure. Meanwhile, the American Welding Society’s 2023 welding workforce data projected demand for 360,000 welding professionals by 2027. Together, these reports point to a practical challenge: production needs repeatable processes and capable people who can recognize when conditions shift.
These spot welding tips focus on checks operators can apply at the machine: verify settings against the approved procedure, inspect electrode tips, keep mating surfaces clean, and watch for consistent weld appearance. A shiny nugget alone proves little. Material thickness, coating, and equipment design matter, so one setting cannot suit every job. Use qualified procedures and equipment guidance. Then record results and investigate variation instead of simply increasing current. Real shop conditions are messier than a checklist, and even a good setup can drift.
How Spot Welding Works and What Affects Weld Quality
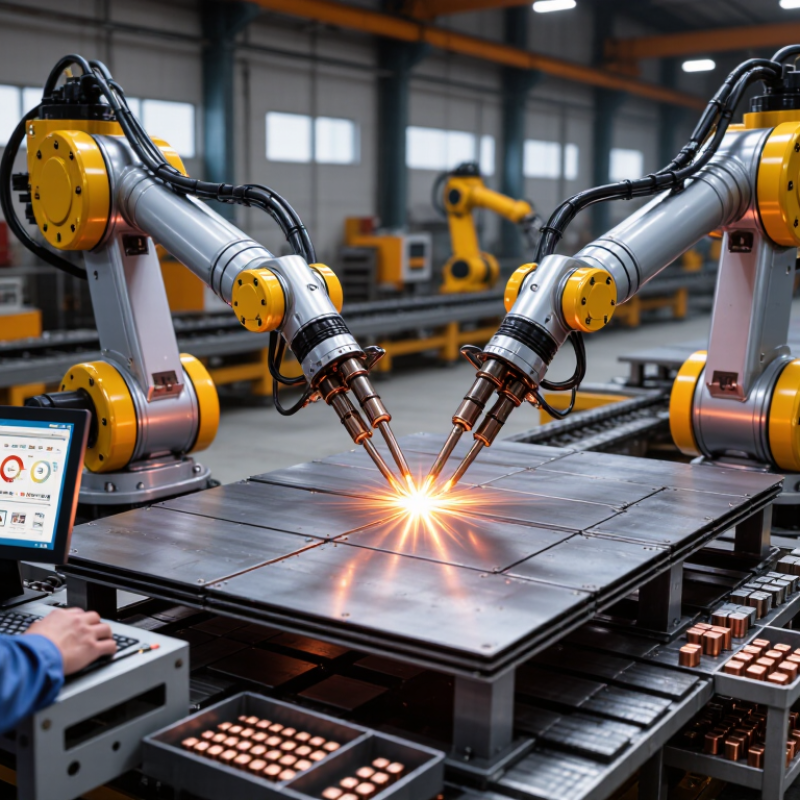
Spot welding joins overlapping metal sheets by passing current through two electrodes. Electrical resistance creates heat at the contact point, while electrode pressure holds the sheets together. The heated area forms a small fused region, often called a weld nugget. The balance matters. Too little heat can leave a weak bond; too much may cause expulsion, deep marks, or damage around the joint.
Weld quality depends on current, weld time, pressure, and the condition of the electrode tips. These settings interact, so changing one can affect the others. Sheet thickness and metal type also matter. Even a thin layer of oil, paint, or rust can change electrical contact and make results inconsistent. Clean surfaces and tight fit-up help the electrodes deliver repeatable pressure. Keep it consistent.
Watch the electrode tips for wear or mushrooming, since their shape affects current concentration. A simple test coupon made from the same material can reveal whether a setting needs adjustment. Inspect the weld for a sound indentation and check sample joints with an appropriate destructive test. Appearance alone is not proof of strength. In practice, a setting that works on one batch may need a small correction on another. That part is easy to overlook.
How to Get Better Welds with These Spot Welding Tips - How Spot Welding Works and What Affects Weld Quality
| Factor | How It Affects Spot Welding | Practical Tip | What to Check |
|---|---|---|---|
| Welding current | Current generates heat at the sheet interface. Because heat generation is approximately proportional to current squared, small current changes can substantially affect the weld. | Use a procedure qualified for the material, thickness, electrode, and machine. Avoid increasing current without checking for expulsion or electrode damage. | A sound weld forms a consistent fused nugget. Excessive current may cause expulsion, surface indentation, or sticking; insufficient current may produce a small or weak nugget. |
| Weld time | Time determines how long heat is generated. Too little time can result in inadequate fusion; too much can increase heat loss, indentation, expulsion, or electrode wear. | Keep the programmed weld time consistent and change it only as part of a tested parameter adjustment. | Look for repeatable weld appearance and destructive-test results rather than relying on appearance alone. |
| Electrode force | Force brings the sheets into contact and contains the molten zone. Too little force can promote arcing or expulsion; excessive force can reduce contact resistance and alter nugget formation. | Set and maintain force according to the qualified welding schedule. Check the mechanism for smooth, repeatable movement. | Check for expulsion, uneven indentation, sheet movement, and variation between welds. |
| Electrode condition and alignment | Worn, contaminated, or misaligned electrode faces change the contact area and current density, making heat and nugget size less consistent. | Inspect and dress or replace electrodes as specified for the process. Confirm that opposing electrode faces meet squarely. | Look for mushroomed tips, deposits, uneven marks, and welds that vary across the part. |
| Sheet fit-up and clamping | Gaps, poor contact, or movement between sheets disrupt current flow and can cause inconsistent fusion or expulsion. | Keep mating surfaces in close contact and fixtures rigid. Place the weld where the electrode can reach both sheets evenly. | Check for gaps, oil-canning, movement during the weld, and variation in electrode indentation. |
| Material, thickness, and coatings | Electrical resistance, thermal conductivity, thickness, and surface coatings all affect heat generation and heat flow. Different material stacks may need different schedules. | Use parameters qualified for the actual materials and layer stack. Do not assume a schedule transfers unchanged to a different coating or thickness. | Confirm the material specification and thickness; validate changes with representative test pieces. |
| Surface cleanliness | Oil, scale, rust, and other contamination can make electrical contact inconsistent and affect weld repeatability. | Follow the material and process requirements for surface preparation. Keep electrodes and work surfaces free of buildup. | Inspect for contamination, erratic weld marks, and inconsistent results across otherwise similar parts. |
| Cooling and production consistency | Electrode cooling and stable machine operation help control electrode temperature and limit changes during repeated welding. | Maintain the specified cooling flow and machine settings; investigate changes in weld quality during long production runs. | Monitor for overheating, increasing electrode wear, and quality drift over successive welds. |
| Weld verification | Appearance alone cannot confirm internal nugget size or joint strength. A weld can look acceptable while lacking sufficient fusion. | Use the inspection and destructive-test method required by the applicable procedure or standard, such as a peel or chisel test where appropriate. | Compare nugget formation, failure mode, and consistency with the approved acceptance criteria. |
Note: Spot-welding settings are material-, thickness-, electrode-, and equipment-dependent. Establish and verify a qualified schedule for the specific application rather than treating any single setting as universal.
Related Posts
-
2026 Best Mini Spot Welding Machine Options for Every Need?
-

2025 Best Spot Welder Guide for Homeowners and DIY Enthusiasts
-
Top 10 Spot Welder Machines for Global Buyers 2026?
-
Top 10 Welding Repair Services for Global Buyers
-
Top 10 Welders in China for Quality and Innovation?
-
10 Best Mobile Welding Services for Your Project Needs?

Contact us
Please fill out the enquiry form, and our dedicated team will promptly attend to your request